For device teams deciding who should mold the part the device cannot function without.
Since 1980, we have done one thing: mold the components medical devices cannot function without. Forty-five years is long enough to have carried programs from a first article to hundreds of millions of parts, and to know exactly what breaks in between.
A valve that opens at the wrong pressure, or a seal that takes a set, can stop a program as surely as a failed circuit board. The part is a rounding error on the bill of materials and one hundred percent of the function.
It fails an audit, gets acquired, exits the niche, or simply cannot scale with the program.
Engineering teams chase root causes. Validation gets repeated. Qualifying a new molder becomes a project of its own.
Every week of requalification is a week the device is not shipping, for a part that costs cents.
IRP Medical exists to take that risk off your team. We take ownership of the four things every quality part requires, then hold that process steady for the life of your device. Qualify once. Scale for the life of the device.
Every serious molder has presses, engineers, and a certificate on the wall. The difference is what the company is built to serve.
Built for enormous automated programs. A two-hundred-thousand-piece Class II component is a rounding error to them.
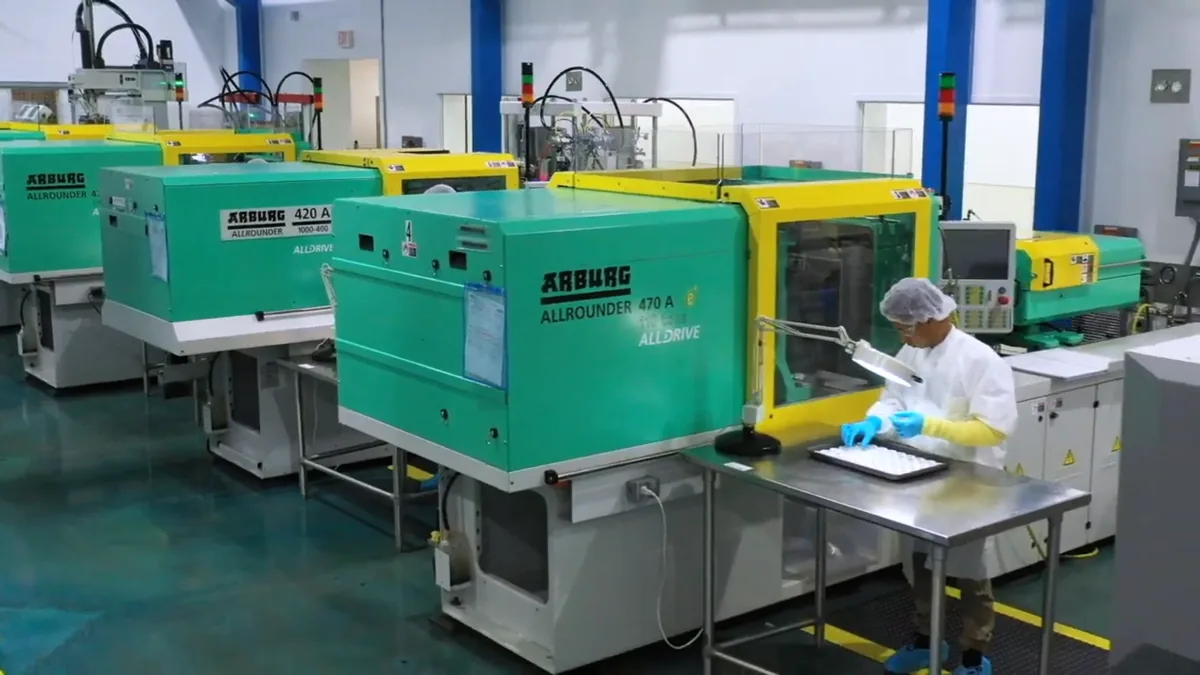
One engineering team, one ISO 13485 quality system, and one press-based floor running everything from ten-piece first articles to high-volume automated cells. The supplier you qualify for your clinical build is the supplier you still have at full commercial volume.
Can take the small job, but cannot scale it or survive a medical audit.
Most device programs live in between: launching in the tens of thousands, heading toward commercial scale, and needing a partner that takes both ends seriously.
Highly rated on customer quality scorecards.
We start with what your part has to do, not just what is on the print. DFM, tolerance guidance, and material recommendations happen before a mold is cut.
We tell you what is realistic for your geometry and material, and how we will control it in production. If a part cannot be made right, we say so up front, before it costs you time.
The engineers who develop your part are the team that runs it. Nothing gets lost in a handoff.
Including the medium and lower volumes larger suppliers often pass on, with a planned, staged path as your forecast grows.
We own the tooling process, from requirements and design through vendor management, validation, and transfer. You never deal with a toolmaker.
Once your part is validated, it is documented, controlled, and traceable under our ISO 13485:2016 quality system, so the part you approved is the part you keep receiving.
At a global supplier, a mid-volume program is one account among thousands. Here, it is a program the plant leadership knows by name.
Our operating partners bring more than twenty-five years each in the industry, and the people who run the floor join the customer calls. One U.S. site means one team, one quality system, and one place to audit. And when a program needs it, the floor runs 24/7.
Precision molding is not just equipment. It takes engineers, technicians, quality specialists, and operations people who understand elastomers and medical devices: how a material behaves in a mold, how a process drifts, and how to catch a problem before it becomes a nonconformance.
Stefan leads IRP Medical with a focus on operational excellence and continuous improvement, drawing on a career across aerospace, automotive, and food and beverage manufacturing.
LinkedInHector is the technical voice behind many of our customer programs, with deep experience in silicone molding and process development.
LinkedInJon brings a career spent in medical device manufacturing and helps device teams find the right path for new programs and supplier transfers, from first conversation through production.
LinkedInAshley keeps active programs moving, from orders and scheduling to day-to-day customer communication, drawing on her background in the medical device industry.
LinkedIn
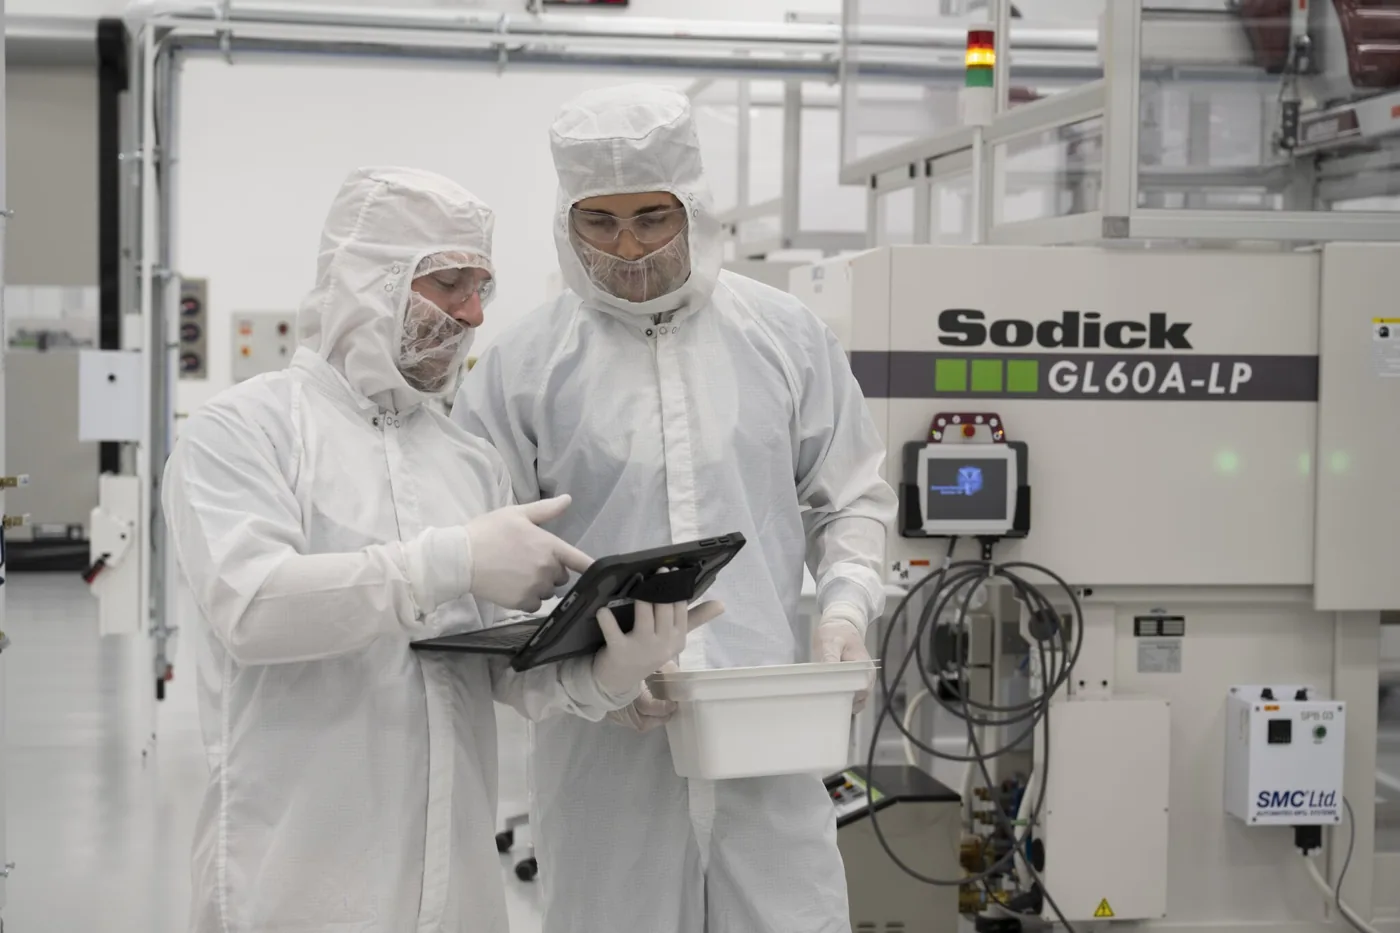
IRP Medical operates from San Clemente, California. Our facility is ISO 13485:2016 certified and FDA registered, with molding in a certified ISO Class 8 cleanroom environment, and 24/7 operations when programs require it.
1035 Calle Amanecer, San Clemente, CA 92673IRP starts in Rancho Dominguez, CA, with its first plant.
ISO 13485 certification.
San Clemente, CA.
Whether you are starting a new device or moving an existing program, you will be talking to engineers from the first message.
From clinical builds to commercial scale, engage our engineers at the print.
Start Your ProgramRevalidation is a given. We plan it around your inventory bank, so your line keeps running while we qualify.
Transfer Your Program